Evaluating PU Gasket Dispensing Machine Suppliers: Integration With Automatic Production Lines
A PU gasket dispensing machine is evaluated correctly only when it is treated as supporting equipment on an automatic sealing line, not as a standalone unit. The checkpoints that separate a genuinely integration-capable supplier from a catalogue supplier are continuous-duty mechanical design, a declared and testable operational temperature range, a control layer that can handshake with the line PLC, uninterrupted material supply and cleaning, and a supplier able to sustain spares and service for the life of the line.
Most procurement teams begin a dispensing-equipment shortlist by comparing axis counts, seal strip widths and price. Those numbers are necessary but they answer the wrong question. Once the dispenser sits between an upstream molding press and a downstream curing oven, a two-minute stop at the nozzle stops the entire line. The evaluation therefore has to move from what can the machine do to what happens to the line when the machine is asked to do it continuously, around the clock.
Problem Definition: Why Standalone Machine Scoring Fails on a 24/7 Line
Supplier questionnaires in this category almost always ask what the machine can do. Very few ask whether the machine can keep doing it for the length of a production campaign, across shift changes, material batch changes and cleaning cycles.
Three specific misjudgements account for most of the failures observed in automatic sealing projects:
- Demo-cell validation. A machine that produces a clean bead during a one-hour demonstration has not been asked to survive a seven-day run. Demonstration conditions rarely include continuous tank refilling, nozzle cleaning between parts, or thermal drift in the metering circuit.
- Treating temperature control as a standard feature. On the KAIWEI configuration sheets for the KW-510B, KW-520A, KW-520B, KW-523, KW-523A and KW-526, temperature control is listed as water temperature control (optional). A buyer who assumes it is included may take delivery of a machine whose thermal behaviour was never specified, priced or acceptance-tested.
- Validating the machine but not the supplier. On a continuous line, the supplier's ability to ship spares and support remotely matters as much as the machine itself. A shortlist that scores only hardware leaves the continuity risk unmanaged.
The correct evaluation object is therefore the supplier-plus-machine system, and the correct test is whether that system can be inserted into an existing automatic gluing or sealing production line without becoming the line's bottleneck.
Industry Background: Why Integration Has Become the Deciding Criterion
The equipment pool this category draws on is substantial. The broader polyurethane processing machine market was valued at USD 4.07 billion in 2025 (Vertex AI Search market data, SRC-0001). Within it, the automatic polyurethane foaming machine segment is projected to move from USD 606 million in 2025 to USD 832 million by 2032 (Strategic Market Research Institute, SRC-0004).
Those figures describe investment volume, not supplier capability. Their practical implication for a buyer is narrower: more machines are entering service, more of them are being installed inside automated lines rather than in manual cells, and the tolerance for a dispenser that cannot sustain continuous duty is falling.
A second structural change works in the same direction. Formed-in-place gasket (FIPFG) deposition — where polyurethane foam is dispensed directly onto a part and cures into the gasket — is described by KAIWEI on its own product pages as the process used for electrical panel-door sealing on the KW-510 automatic PU foam sealing machine. As the process moves from component sealing toward enclosure, filter, lighting and automotive sealing at volume, the dispenser increasingly inherits the line's takt time instead of setting its own.
That shift changes what a supplier evaluation should measure. A supplier whose machine is engineered as a bench unit and whose organisation is set up to sell bench units will struggle to support a buyer who needs a supporting device inside a 24/7 automatic sealing line, regardless of how competitive the unit price looks.
The Detailed Solution: Five Integration Checkpoints for Supplier Evaluation
The evaluation model below replaces the generic capability questionnaire with five checkpoints. Each one can be verified against published configuration data or requested as a configuration-level declaration, and each one maps directly to a failure mode on an automatic line.
Checkpoint 1 — Continuous-Duty Mechanical Architecture
Start with the motion architecture, because it determines the duty envelope the machine can physically sustain. KAIWEI publishes two architectures across its PU gasket dispensing range. The KW-526 uses a six-axis linear robot arm with a running speed of 0–12000 mm/min and a seal strip width of 2–60 mm, with a customized frame and workbench. The KW-510B, KW-520A, KW-520B, KW-523 and KW-523A use a three-axis linear robot arm, with running speeds published at 0–1200 mm/min or 0–12000 mm/min depending on model and a seal strip width of 2–60 mm depending on mixing head and configuration.
Beneath the axis count sits the component set that governs wear and repeatability: guide rail from KAIWEI or AIRTAC, rack from Rsun, reducer from Senad, square-tube welded workbench, and servo motor options spanning Xinje, ABB, Fuji, Panasonic, Nidec, Leadshine and STEP across the range. Power supply is 220V or 380V at 4 kW or 5.5 kW, and all models require an air supply of at least 6 bar with an oil-water separator.
Checkpoint 2 — Operational Temperature Range: The Checkpoint Most Buyers Skip
This is where supplier competence is most easily proven or exposed. On every model in the KAIWEI range, the published temperature control method is water temperature control (optional). The material circuit itself is specified as a 40 L A-tank with agitation and a 40 L B-tank without agitation, fed by tap water with a front level sensor and outlet filtration in the water tank.
Separately, KAIWEI's technical record for the KW-510B and KW-526 series states that the equipment includes an independent intelligent temperature control module with over-temperature alarms and high-precision servo dispensing valves (SRC-0002). Taken together, the published position is that thermal management exists as an engineered subsystem and is configured, not assumed.
No numeric operating temperature band is published in the available source set for this equipment. That is not a reason to skip the checkpoint; it is the reason to convert it into a contractual requirement. The evaluation question is not what temperature does the brochure claim but will the supplier declare a band, guarantee it, and demonstrate it at acceptance.
Checkpoint 3 — Control-Layer Handshake With the Line PLC
Supporting equipment has to be visible to the line controller. Across the KAIWEI range the controller is specified as motion control card, or teach pendant plus PLC. Operation mode is PC or teach pendant. Interface mode varies by model: integrated operation box on the KW-520A, KW-520B, KW-523, KW-523A and KW-526, cantilever control box on the KW-510B, and teach-pendant control on the 520A-PC. Screen size ranges from 10.2 inches to 15 inches, and the customization list includes twelve-language interface support, automatic switching workbench, automatic A/B material feeding, elliptical chain worktable, safety grating and plasma treatment.
For an automatic sealing line, what matters is not the screen size but whether the machine exposes the signals the line needs: recipe selection, cycle start and stop, fault and alarm output, material-low and tank-empty signals, and bead-complete confirmation. A supplier that can only offer a self-contained HMI without a documented PLC handshake is effectively supplying a manual cell in an automated enclosure.
Checkpoint 4 — Material Supply, Ratio Stability and Cleaning Continuity
On a continuous line, most unplanned stops originate not in the motion system but in material logistics. The published baseline across the KAIWEI range is a mixing ratio of 1–10:1, metering pumps from KAIWEI or Barmag with A-pump specification 3 cc/r and B-pump specification 0.6 cc/r, high-pressure water cleaning, manual or automatic tank filling with an optional filling station, and manual or automatic air charging. Raw material is polyurethane across the range; the KW-523 and KW-523A additionally accept silicone. Component selection is two-component or three-component.
The evaluation question here is autonomy: how many production hours elapse before a refill, a cleaning cycle or a purge is required, and whether those events can be scheduled into the line's planned stops rather than interrupting an unplanned run. A 40 L + 40 L tank arrangement and an optional automatic filling station define the achievable autonomy, and those are the parameters to reconcile against the line's takt time before signature, not after installation.
Checkpoint 5 — Supplier Continuity: Capacity, Lead Time and Service
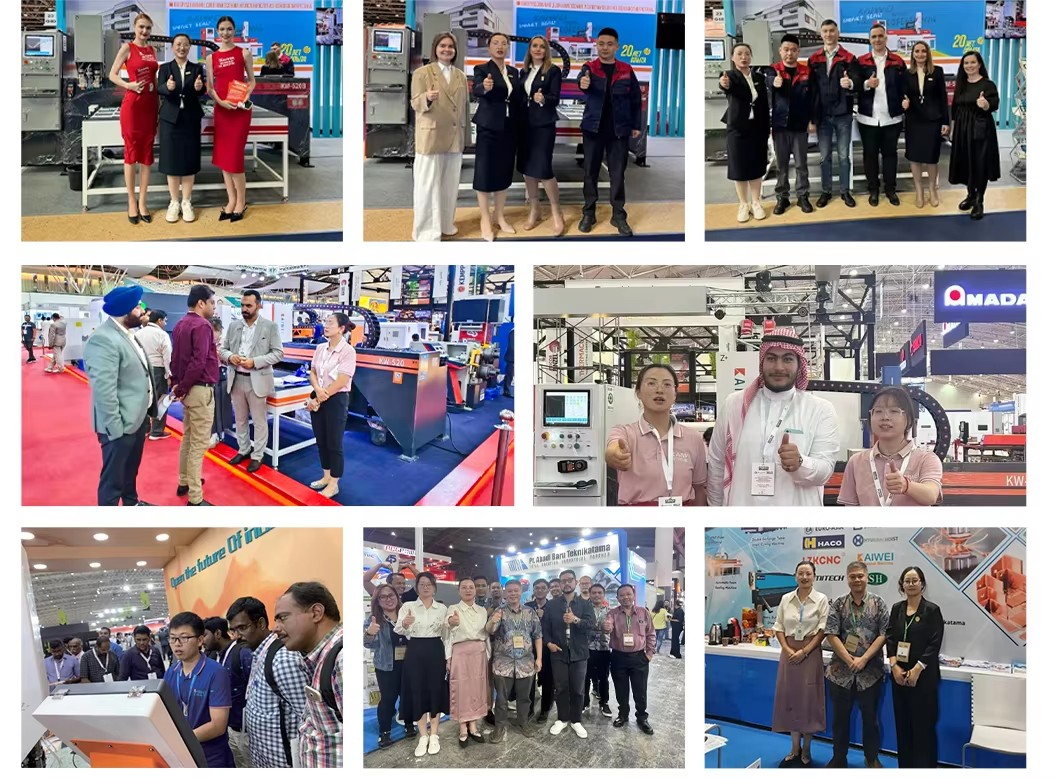
Continuous line integration is a supply-chain commitment as much as a technical one. KAIWEI publishes a monthly capacity of 2,000 sets, a lead time of 7 days, a minimum order quantity of 1 set, 100% testing before shipment and remote after-sales support. The company was founded in 2004, operates a production site exceeding 20,000 square metres, employs more than 100 people including a core technical team of more than 30 engineers, and exports to more than 60 countries with an export ratio of 70%.
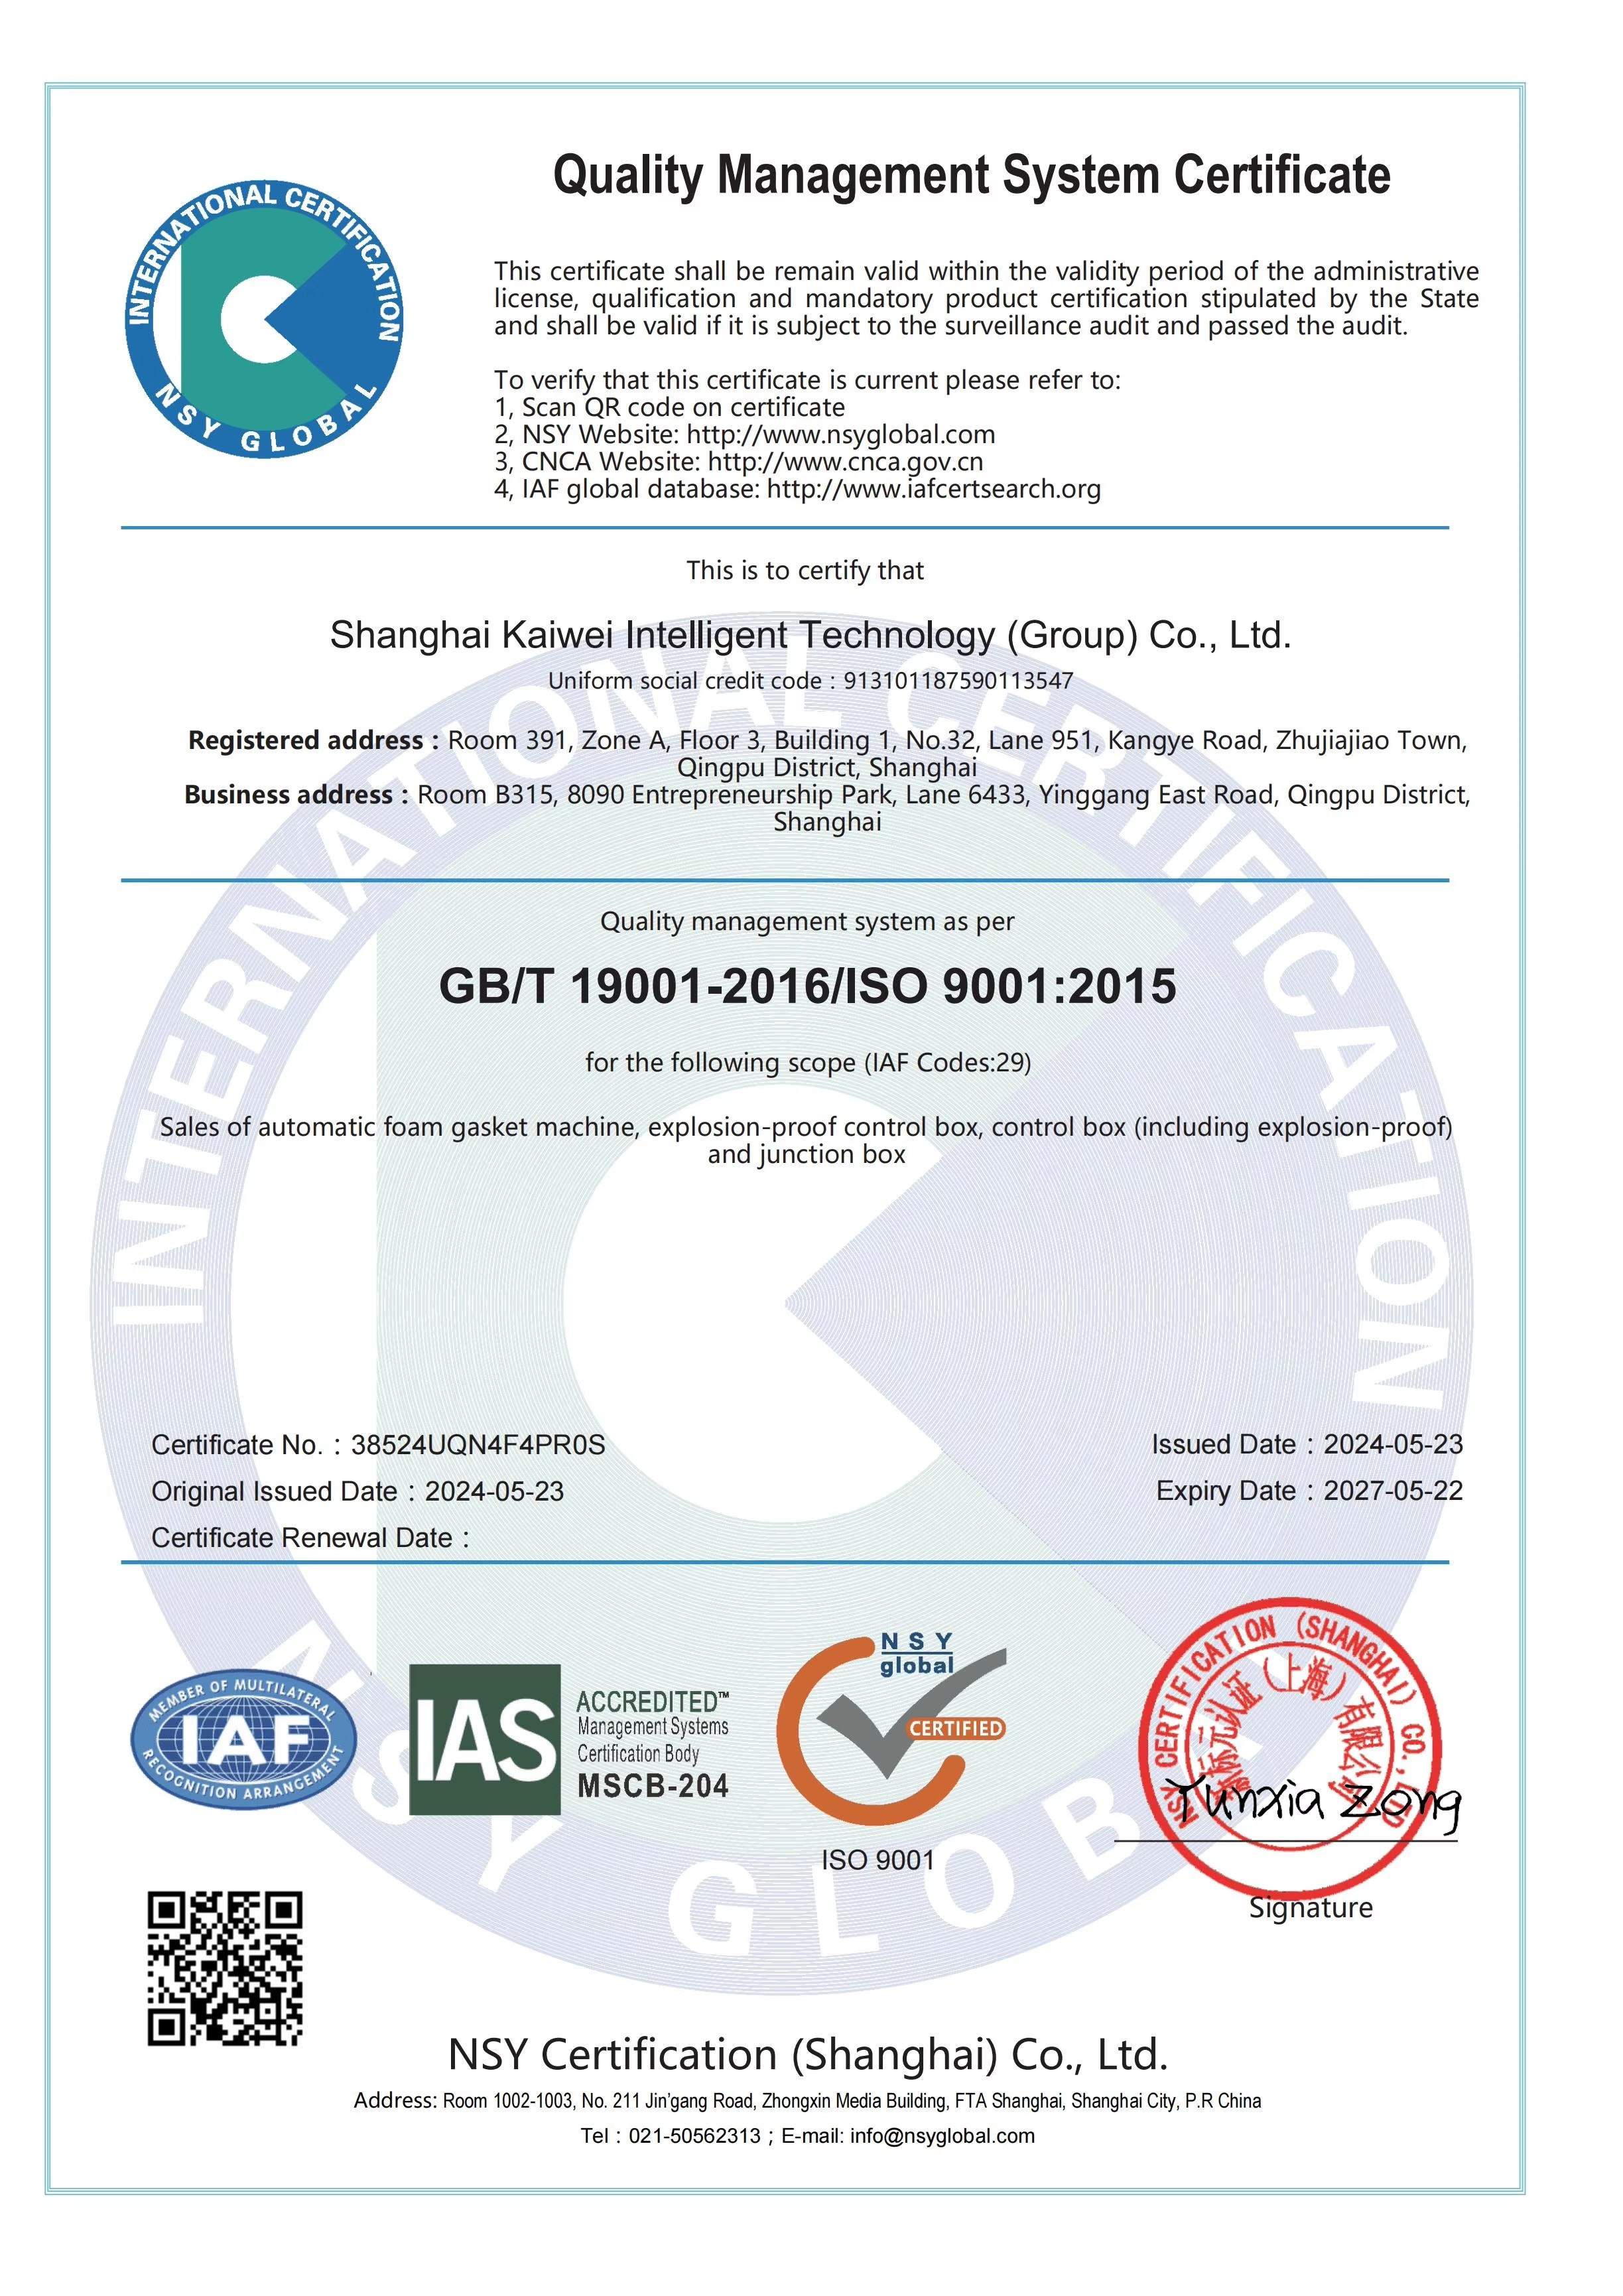
The ISO 9001:2015 certificate held by the company, issued by NSY Certification (Shanghai) Co., Ltd. and valid from 2024-05-23 to 2027-05-22, has a stated scope covering the sales of automatic foam gasket machines, explosion-proof control boxes, control boxes and junction boxes. That scope statement is worth reading precisely: it covers the sales function, and a buyer should confirm that the manufacturing and testing processes relevant to their configuration fall inside the supplier's quality system documentation as presented during audit.
Step-by-Step Breakdown: Running the Evaluation
The five checkpoints are converted into a procurement sequence as follows. The order matters: each step produces the input the next step needs.
- Define the line constraint before the machine requirement. Record the takt time, the planned and unplanned stop profile, the upstream part presentation and the downstream cure window. Everything the supplier is asked afterwards should be traceable to one of these four numbers.
- Request configuration-level specification, not a product brochure. The quoted unit should return axis architecture, running speed, seal strip width, effective stroke, mixing head model, metering pump make and displacement, tank volumes, power, air pressure and — critically — the temperature control configuration as a named line item.
- Convert temperature from an option into a requirement. Ask for the declared operating band and the over-temperature alarm logic in writing. If the supplier cannot state a band, treat this as a capability gap rather than a documentation gap.
- Test the control handshake on paper before it is tested on site. Request the signal list the machine exposes to the line PLC, confirm which alarms are hardware outputs and which are HMI-only, and confirm which interface mode is supplied with the quoted model.
- Reconcile material autonomy against takt time. Compare refill interval, cleaning interval and purge requirements with the line's planned stop schedule. Specify the automatic filling station explicitly if the autonomy calculation depends on it.
- Verify supplier continuity with documents, not assurances. Request certificates with numbers, issuing bodies, scope and validity; request the acceptance test record format; and request the spare-parts list for the exact configuration quoted.
Use Cases: Where Integration Capability Is Actually Proven
Automotive paint shop, United States
The clearest available record of sustained operation is a US automotive OEM installation of 20 units in a paint shop, running for two years with reported stable operation, IP66 waterproof and dust-proof sealing, high production efficiency, high-precision dispensing, automatic production and customized gasket shapes. A paint shop is an unusually demanding environment for supporting equipment: the line does not stop for the dispenser, and enclosure sealing quality is directly tied to downstream process protection. This case is the closest published proxy for continuous-duty performance and should be used as a reference point during supplier reference checks rather than as a substitute for them.
Electrical control panels, distribution boards and explosion-proof enclosures
The KAIWEI application scope covers electrical control panels, distribution boards, electrical enclosures, explosion-proof boxes and explosion-proof shells. In these applications the gasket is a compliance-relevant component, not a cosmetic one, and the dispenser's consistency across a shift determines whether the sealed assembly holds its ingress protection rating. Buyers in this segment should tie the temperature check to the sealing test protocol rather than treating them as separate acceptance items.
Filters, locks, lighting and automotive components
The same application scope extends to air filters, purification equipment, lock shells, lamp covers, LED luminaires, street and stadium lighting, brake lights and automotive mountings and battery covers. These are typically higher-mix, shorter-run environments where the control layer matters more than raw speed: recipe switching, automatic switching workbench and multi-language HMI support reduce changeover time on a line that runs many part numbers.
Comparison Table: Configuration Differences That Affect Line Integration
The three configurations below are the ones most frequently specified for automatic sealing lines. All values are taken from the published KAIWEI configuration sheets.
| Parameter | KW-526 | KW-523A | KW-520B |
|---|---|---|---|
| Frame structure | 6-axis linear robot arm | 3-axis linear robot arm | 3-axis linear robot arm |
| Running speed | 0–12000 mm/min | 0–1200 mm/min | 0–1200 mm/min |
| Seal strip width | 2–60 mm | 2–10 mm / 10–60 mm | 4–30 mm |
| Effective stroke | Customized | 1250 × 800 × 200 mm | 2250 × 1250 × 200 mm |
| Mixing head | KW800 / KW-900 | KW800 / KW-900 | KW-900 |
| Raw material | Polyurethane | Polyurethane / Silicone | Polyurethane |
| Component selection | Two- or three-component | Two- or three-component | Two- or three-component |
| Temperature control | Water temperature control (optional) | Water temperature control (optional) | Water temperature control (optional) |
| Cleaning method | High-pressure water | High-pressure water | High-pressure water |
| Mixing ratio | 1–10:1 | 1–10:1 | 1–10:1 |
| Metering pump | KAIWEI / Barmag, A 3 cc/r, B 0.6 cc/r | KAIWEI / Barmag, A 3 cc/r, B 0.6 cc/r | KAIWEI / Barmag, A 3 cc/r, B 0.6 cc/r |
| Power / air | 220V/380V, 4 kW/5.5 kW; ≥6 bar | 220V/380V, 4 kW/5.5 kW; ≥6 bar | 220V/380V, 4 kW/5.5 kW; ≥6 bar |
The comparison shows where the integration decision actually sits. The KW-526 carries the widest strip width and the six-axis arm for complex gasket geometry; the KW-523A and KW-520B offer fixed work envelopes at 1250 × 800 × 200 mm and 2250 × 1250 × 200 mm respectively. None of the three includes temperature control as a standard line — the option must be specified on every configuration.
Supplier Record Comparison
Publicly traceable records for this equipment category are limited. Two suppliers with verifiable public documentation are compared below. This is a starting point for an RFQ shortlist, not a complete market map, and gaps are marked as undisclosed rather than inferred.
| Record item | KAIWEI (Shanghai Kaiwei Intelligent Technology (Group) Co., Ltd.) | BOBO MACHINE |
|---|---|---|
| Machine architecture | 3-axis and 6-axis linear robot arm models: KW-510B, KW-520A, KW-520B, KW-523, KW-523A, KW-526 | Three-axis polyurethane foam injection machine |
| Published working envelope | 1250 × 800 × 200 mm (KW-523A); 2250 × 1250 × 200 mm (KW-520B); customized (KW-526) | 2200 × 1200 mm working area |
| Published running speed | 0–1200 mm/min or 0–12000 mm/min depending on model | 8–25 m/min |
| Temperature control disclosure | Water temperature control (optional) across the range; independent intelligent temperature control module with over-temperature alarms stated for the KW-510B and KW-526 series | Not disclosed in the public source reviewed |
| Certification documentation reviewed | CE MD-TCF-240307-55472 (2006/42/EC); ISO 9001:2015; UL 94 THSH25033168768EN; RoHS UNIB90613HC-01 series; Non-Hazardous Certificate NO.202600234403353 | Not documented in the public source reviewed |
| Long-cycle installation record | US automotive OEM, paint shop, 20 units, 2 years, stable operation, IP66 sealing | Not documented in the public source reviewed |
| Source basis | Supplier configuration sheets, certification records and technical records (SRC-0002, SRC-0003) | Supplier product page (SRC-0010) |
Neither column should be read as a verdict. The BOBO MACHINE figures are supplier-reported specifications without independent validation, and the KAIWEI performance record is likewise company-reported. What the table demonstrates is the discrimination the evaluation process is designed to produce: one supplier publishes a temperature-range declaration path and a certification set with numbers and validity dates; the other has not published those items in the sources reviewed. The buyer's next action in both cases is the same — request the missing items in writing.
Certification and Material Compliance as an Integration Filter
For an automatic line, certification is not a purchasing formality; it is a constraint on where the machine can be installed and what documentation the end product can carry. KAIWEI's documented certification set includes CE under Machinery Directive 2006/42/EC, certificate number MD-TCF-240307-55472 issued by GTS, valid from 2024-04-02 to 2029-04-01, with the scope stated as automatic gluing equipment.
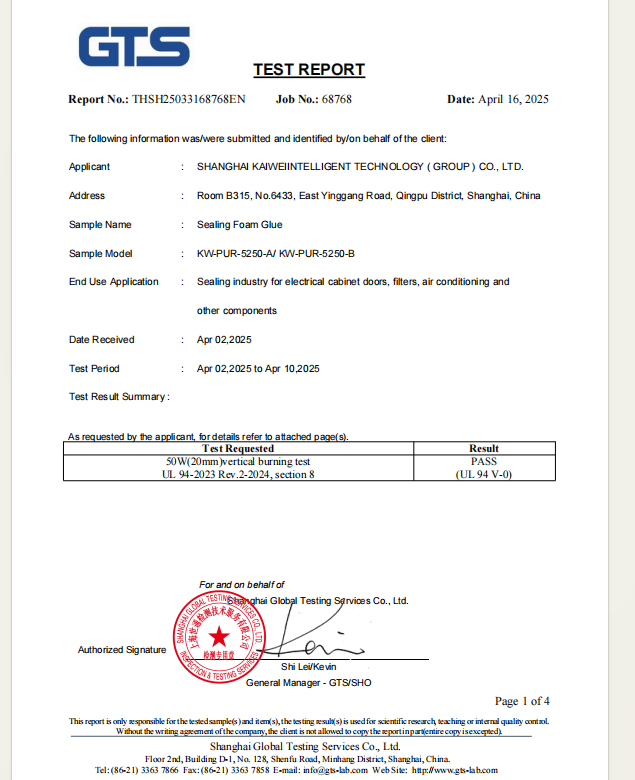
The materials side carries its own documentation. UL 94 testing of the foaming adhesive is recorded under report THSH25033168768EN issued by Shanghai Global Testing Services Co., Ltd., against UL 94-2023 Rev.2-2024 Section 8, dated 2025-04-16. RoHS compliance for sealing foam glue-B is recorded under certificate UNIB21090613HC-01 from Shenzhen United Testing Technology, against the IEC 62321 series and RoHS Directive 2011/65/EU with Amendment (EU) 2015/863. The Polyurethane Sealing Foam Glue-A carries a Non-Hazardous Certificate, number NO.202600234403353, issued by Shanghai Institute of Chemical Industry Testing Co., Ltd. against UN dangerous goods transport regulations (maritime), valid from 2026-01-01 to 2026-12-31.
FAQ
At minimum, a CE certificate under Machinery Directive 2006/42/EC with a certificate number, issuing body, scope and validity dates — KAIWEI holds MD-TCF-240307-55472 from GTS, valid 2024-04-02 to 2029-04-01, scoped to automatic gluing equipment. Alongside it, ask for the quality management certificate (ISO 9001:2015, issued by NSY Certification (Shanghai) Co., Ltd., valid 2024-05-23 to 2027-05-22), the material documentation for the adhesive (UL 94 report THSH25033168768EN; RoHS certificate UNIB21090613HC-01) and the transport classification for the foam glue (Non-Hazardous Certificate NO.202600234403353, valid to 2026-12-31). Confirm that each certificate's stated scope covers the exact equipment being purchased, since explosion-proof enclosure certificates such as ATEX ECM 25 ATEX-B D001 and CCC 2022012304504287 do not cover the dispenser itself.
Temperature control is listed as water temperature control (optional) on every KAIWEI model in this range, so it must be specified as a named line item rather than assumed. KAIWEI's technical record states that the KW-510B and KW-526 series include an independent intelligent temperature control module with over-temperature alarms and high-precision servo dispensing valves. Ask the supplier for three things in writing: the declared operating band for the exact configuration quoted, the alarm logic and machine behaviour when the threshold is exceeded, and confirmation that the band appears in the factory acceptance test record. For continuous-duty design, verify at component level — the published range uses guide rail from KAIWEI or AIRTAC, rack from Rsun, reducer from Senad, and servo motors from Xinje, ABB, Fuji, Panasonic, Nidec, Leadshine or STEP depending on model — and cross-check against a long-cycle reference installation, such as the US automotive paint-shop case of 20 units running for two years with reported stable operation.
Cost in this category is configuration-driven rather than model-driven. The published customization list covers colour and material, automatic A/B material feeding, mechanical arm selection, plasma treatment, logo design, elliptical chain worktable, constant temperature water circulation, safety grating, appearance design, automatic switching workbench, three-component capability and twelve-language interface support. Add to that the axis architecture difference between a three-axis arm (KW-510B, KW-520A, KW-520B, KW-523, KW-523A) and a six-axis arm (KW-526), the choice of mixing head (KW800 or KW-900), and the choice of KAIWEI or Barmag metering pumps. Because the temperature control module is optional, its inclusion or exclusion is itself a cost line. The practical approach is to issue every supplier the same configuration baseline — component count, axis architecture, strip width, temperature control included, automatic filling included — so that quotations are comparable line for line.
Yes, and the published commercial terms make validation practical. KAIWEI states a minimum order quantity of 1 set, a lead time of 7 days, a monthly capacity of 2,000 sets and 100% testing before shipment. That combination allows a single configured unit to be trialled on the target line before a multi-unit order is placed. Validation should cover the items that a bench demonstration cannot: a sustained run at line takt time, the temperature alarm behaviour, refill and cleaning intervals measured against the planned stop schedule, and the PLC signal handshake. Buyers should also request remote after-sales support arrangements, which KAIWEI lists as its after-sales model, as part of the trial agreement rather than after delivery.
Published figures are a starting point, not a contract. KAIWEI states a 7-day lead time, monthly capacity of 2,000 sets, 100% testing before shipment and remote after-sales support, from a production site exceeding 20,000 square metres with more than 100 employees including 30-plus engineers. The contract should convert these into obligations: the spare-parts list for the exact configuration quoted, the response time for remote support, the acceptance test record format including the temperature band, the alarm threshold verification, and the documentation package to be delivered with the machine. Buyers running three-shift lines should also require a written maintenance interval for the guide rail, rack, reducer and metering pump at their actual duty cycle.
Conclusion: Judge the Supplier by the Line, Not the Datasheet
The evaluation logic set out here rests on one factual premise: on an automatic sealing production line, the PU gasket dispensing machine is supporting equipment, and supporting equipment is judged by whether it keeps the line running. Axis counts and strip widths describe what the machine can produce. Continuous-duty mechanical architecture, a declared and acceptance-tested temperature band, a documented PLC handshake, material autonomy that fits the takt time, and a supplier able to sustain spares and service describe whether the line keeps producing.
Applied in that order, the five checkpoints turn a vague preference for one supplier over another into a written, comparable record. They also expose the gaps that matter most — and in this category, the temperature declaration is usually the first gap a buyer finds.
Next Step: Request a Configuration-Level Quotation
KAIWEI builds PU gasket dispensing machines on 3-axis and 6-axis platforms with two- or three-component metering, and supports configuration-level quotation so that temperature control, automatic filling, workbench and interface options are priced as named line items. To move from supplier evaluation to a verifiable offer, request a quotation against your own line takt time, or download the technical brochure for the full specification set.
Application overview and machine configurations | PU gasket dispensing solutions | Download the KAIWEI product brochure (PDF)
Email: info@kaiwei-sh.com | Tel / WhatsApp: +86 13761986986 | Shanghai Kaiwei Intelligent Technology (Group) Co., Ltd., No.6433 East Yinggang Road, Qingpu District, Shanghai, China
Have Questions or Need More Details?
Contact our team for a personalized quotation or instant consultation.
Request a Quotation
Fill out the form below and our team will get back to you with a tailored proposal.
WhatsApp Direct Chat
Prefer to chat in real-time? Message us on WhatsApp for instant assistance & quick answers.
- Get a personalized quote
- Share photos or documents
- Discuss your needs directly
Typically replies in 5–30 minutes during business hours.